Plastic Recycling Line Trends for Mixed Waste
Plastic recycling line trends show a move toward tighter sorting, multi-material melt processing, and smart control. Buyers should plan for flexible lines that handle contamination, reduce rework, and integrate automated quality checks.
- Mixed plastic lines are shifting from single-material focus to flexible multi-material processing.
- Sorting accuracy is rising because downstream quality depends on input consistency.
- Melt processing is moving toward multi-material melt lines and advanced filtration.
- Pelletizing is adding inline quality control and better control of melt index and color.
- Buyers should prioritize modularity, data access, and service support over maximum throughput.
Why mixed plastic is changing line design
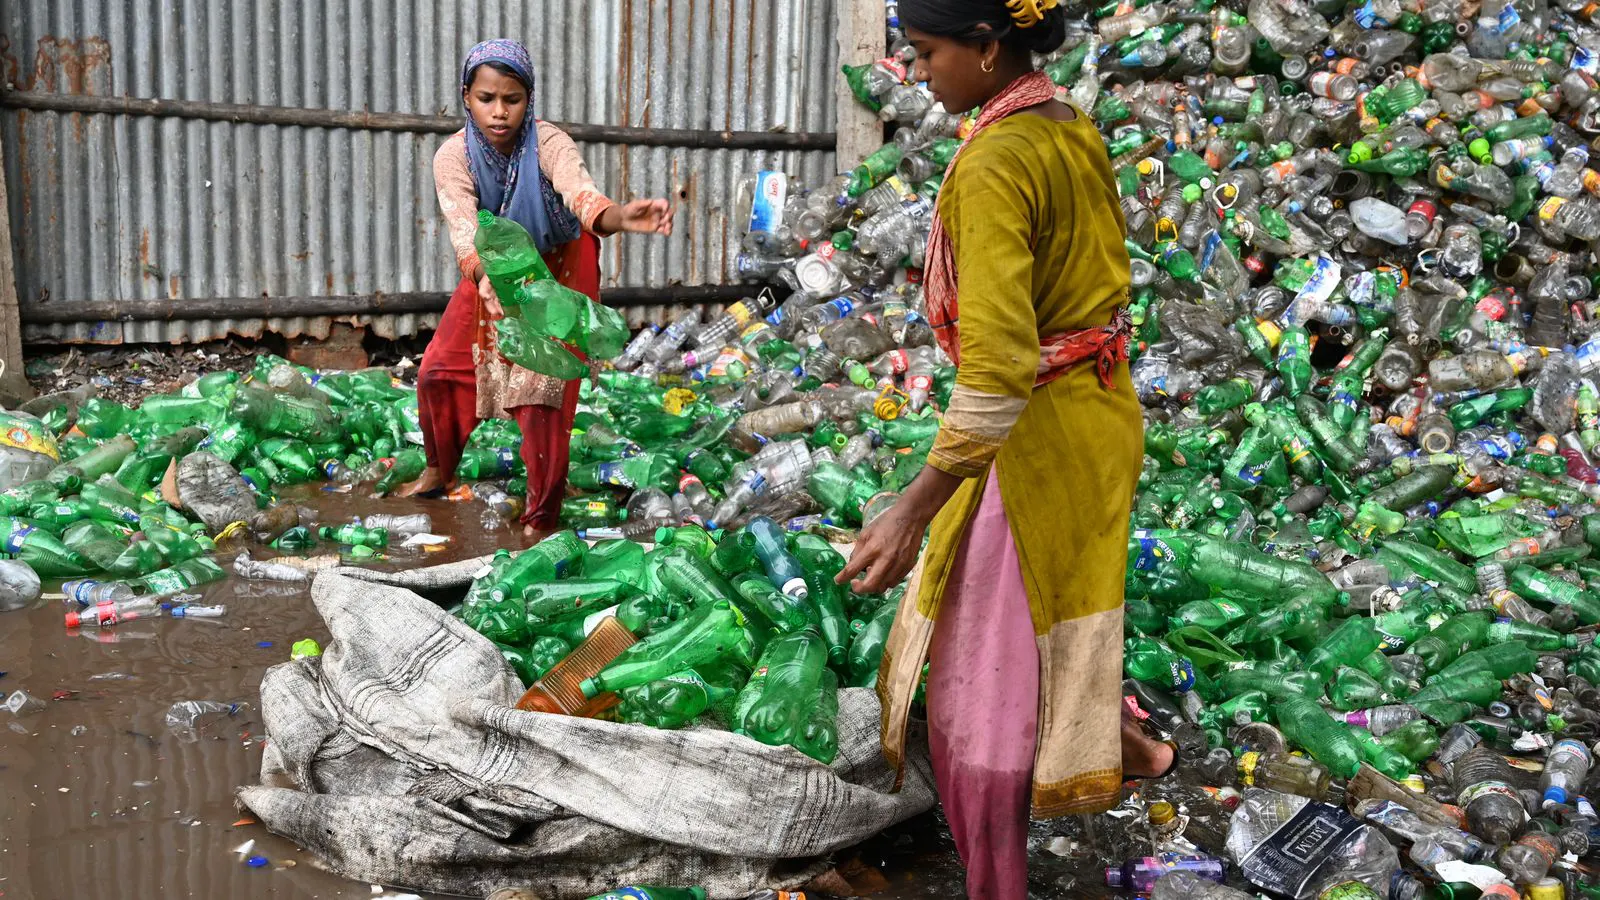
Mixed plastic recycling lines used to be built around one assumption: the input stream is fairly consistent. In practice, that assumption is failing. More mixed plastic waste is entering the market, and the waste is more varied. This is pushing equipment designers and line integrators to rethink how sorting, washing, and pelletizing work together.
The result is a set of practical shifts that buyers should plan for now. These are not speculative. They are already visible in line configurations, control systems, and the way machines are sold.
Sorting is getting tighter
The first shift is in sorting. Older lines relied on coarse separation and accepted a lot of variability. Newer lines use more precise separation and tighter quality gates.
This matters because sorting determines everything downstream. If the sort is weak, the wash tank carries more contamination. If the wash tank carries more contamination, the extruder sees more stress. If the extruder sees more stress, the pellet line runs hot and the quality control team fights the same problem every shift.
Buyers should look for lines that sort by material class, not just by size or color. That means clear separation of polyethylene, polypropylene, and other common grades. It also means removing non-plastic items before they reach the melt.
A practical check is to ask for a sample feed. Run a known mixed waste batch through the sorting stage and inspect the output. If the sort is weak, the pelletizing line will suffer.
Melt processing is moving toward flexibility
The second shift is in melt processing. Mixed waste lines are moving away from single-material extrusion toward multi-material melt processing. This is not just a marketing term. It changes how the line is sized and how the control logic works.
In a single-material line, the extruder profile is tuned for one resin. In a mixed waste line, the melt may contain different resin behaviors at different times. The line needs to handle that variation without constant manual intervention.
This is where equipment choices matter. Melt processing lines are adding better melt index control, better filtration, and better temperature stability. The goal is to keep the melt consistent even when the input changes.
A good test is to ask how the line handles a shift in resin blend. For example, if the feed changes from a polyethylene rich mix to a polypropylene rich mix, how quickly can the line stabilize? The answer should be specific. It should include the control method, the expected time, and the quality checks that confirm stability.
Pelletizing is adding inline quality control
The third shift is in pelletizing. Pelletizing is no longer just a cutting step. It is becoming a quality control point. This is especially true for mixed waste, where resin quality can vary from batch to batch.
Modern pelletizing technology is adding inline checks. These can include melt temperature, pressure, density, and color. The point is not to add more screens. The point is to catch problems before they become finished product.
For buyers, this changes the value of the pelletizing section. A line that only produces pellets is less useful than a line that produces pellets with consistent properties. The latter is easier to sell, easier to store, and easier to use in downstream processing.
A practical question is whether the pelletizing section records data in a way that can be reviewed after production. If the data is only on a local screen, it is useful for the shift operator. If the data is accessible for review, it is useful for the buyer.
Control systems are becoming the differentiator
The fourth shift is in control. Old lines were controlled by operators who knew the machine by feel. Newer lines are controlled by integrated systems that monitor multiple variables at once.
This is not about adding more buttons. It is about reducing the number of places where a problem can hide. When a line has too many manual controls, a small change in feed can create a large problem in the output. When the controls are integrated, the system can respond to small changes before they become big problems.
Buyers should look for a control system that can handle the full line, not just the extruder. That includes the feeders, the washers, the melt section, and the pelletizer. The system should show the relationship between the input and the output.
A simple test is to ask for a demo with a known mixed waste feed. Watch how the line responds when the feed changes. If the response is slow or requires manual correction, the control system is not doing its job.
Line modularity is becoming a planning requirement
The fifth shift is in line design. Buyers are moving away from fixed lines toward modular designs. This is not just a preference. It is a planning requirement.
Mixed waste lines face changing input. The mix of resins changes. The contamination level changes. The wash requirement changes. A fixed line struggles with that. A modular line can be adjusted without a full rebuild.
Modularity means that the sorting, washing, and pelletizing sections can be changed or upgraded without replacing the whole line. It also means that the line can be reconfigured for different waste streams.
For buyers, this changes the purchase decision. The cost is not just the equipment. It is the ability to change the line as the market changes. A line that cannot be modified is a risk.
How to prepare for these shifts
The final shift is in buyer behavior. Buyers who only look at throughput are missing the point. The real question is whether the line can handle the feed it will actually see.
A practical preparation plan has three steps. The first is to define the feed. This means knowing the resin mix, the contamination level, and the wash requirement. The second is to test the line with that feed. This means running a known batch through the full line and checking the output. The third is to review the data. This means checking whether the line records the variables that matter.
A table helps here. It shows the key decision points and the questions buyers should ask.
| Decision Point | What to Check | Why It Matters |
|---|---|---|
| Sorting | Material class separation | Determines downstream quality |
| Washing | Residue removal | Affects melt stability |
| Melt Control | Blend handling | Determines output consistency |
| Pelletizing | Inline quality checks | Determines finished product quality |
| Control System | Integrated monitoring | Reduces manual correction |
| Modularity | Upgrade path | Protects against feed changes |
A short checklist for buyers
Use this checklist when evaluating a mixed waste line:
- Run a known mixed waste feed through the full line.
- Check the sort output for material class accuracy.
- Check the wash output for residue removal.
- Check the melt output for stability when the feed changes.
- Check the pellet output for consistent properties.
- Check the control system for integrated monitoring.
- Check the data access for review after production.
- Check the service support for the specific line configuration.
What buyers should avoid
Buyers should avoid lines that are sold on throughput alone. A line that produces 10 tons per hour but produces inconsistent pellets is less useful than a line that produces 7 tons per hour with consistent properties.
Buyers should also avoid lines that require constant manual adjustment. If the line needs an operator to tune every shift, the control system is not doing its job.
Buyers should avoid lines that do not record data. If the line cannot show what happened during production, it is harder to troubleshoot problems and harder to improve quality.
The bottom line
The direction is clear. Mixed plastic lines are moving toward tighter sorting, more flexible melt processing, and better inline quality control. The buyers who plan for this are the ones who get a line that works with their feed, not a line that fights it.
The practical step is to test the line with your feed. That is the only way to know if the line will work for your situation.
Frequently asked questions
What is the biggest change in mixed plastic lines?
The biggest change is the move from single-material focus to flexible multi-material processing. This changes how sorting, washing, and pelletizing are designed.
How do I test a mixed waste line before buying?
Run a known mixed waste feed through the full line. Check the sort output, the wash output, the melt output, and the pellet output. Then review the data.
Is modularity worth the extra cost?
Yes, if the feed changes over time. Modularity allows the line to be adjusted without a full rebuild. It protects against feed changes.
What should I look for in the pelletizing section?
Look for inline quality checks and data access. The pelletizing section should record melt temperature, pressure, density, and color.
How do I know if the control system is good?
Watch how the line responds when the feed changes. If the response is slow or requires manual correction, the control system is not doing its job.